Hey folks, let’s cut to the chase—if you’re here, it’s probably because your gate valves are leaking, sticking, or just not holding pressure like they should. And let’s be real, as a gate valve supplier, I’ve seen way too many ops teams run into avoidable headaches because they skip the small, impactful steps to boost sealing performance. I’m not gonna hit you with a bunch of jargon that makes your eyes glaze over—this is straight from the shop floor, the stuff that actually works, not the textbook fluff. Gate Valve
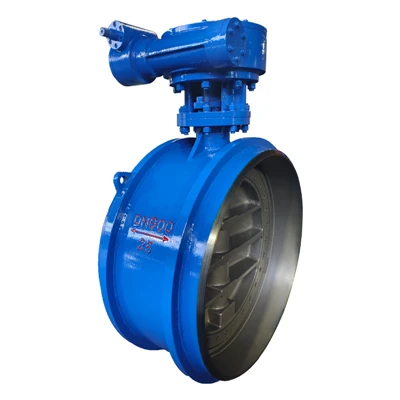
First off, let’s get one thing straight: gate valves don’t seal by magic. Their whole schtick is a wedge-shaped gate that presses against two seat rings (usually metal or rubber) to block flow. If any part of that system is off, leaks happen, and trust me, leaking valves aren’t just annoying—they’re a safety hazard, waste money, and can tank your process efficiency. Over the years, I’ve had customers come to me saying their brand new valves are already leaking, and 9 times out of 10, it’s not a factory defect—it’s how they install, maintain, and operate ’em.
Let’s start with installation, because that’s where 50% of sealing issues start. I see guys rushing through the job, cranking bolts too tight or too loose, and that’s a rookie mistake. The seat rings are mounted into the valve body with bolts, right? If you over-tighten those, you’ll warp the seat ring—think of a paper plate bent too far, it won’t lay flat against the gate. If you under-tighten, there’s a gap between the seat and body, so fluid seeps out around the seat. What’s the sweet spot? We always tell customers to use a torque wrench, and match it to the seat material. For metal seats, that’s usually 25 to 35 ft-lbs, for soft seats (like EPDM or Buna-N), drop it to 15 to 20 ft-lbs. Way too many guys skip the wrench and just “tighten till it feels right”—bad call.
Then there’s pipe alignment. Oh man, this is the big one I see on big installations. If your pipe isn’t perfectly aligned when you bolt the valve flanges on, that’s pulling the valve body out of whack, so the gate can’t seat evenly. It’s like trying to close a door when the frame’s crooked—one side won’t lock. I had a refinery customer a few months back that had 12 gate valves leaking 24/7, turns out their pipe fitters left a 1/8 inch gap between the flange and valve, so when they tightened the bolts, the valve body warped. They fixed it with a couple of alignment clamps, torqued the bolts properly, and all the leaks stopped. Pro tip: use a straightedge to check the flange alignment before you attach the valve. If there’s any gap more than 1/16 inch, adjust the pipe. No shortcuts here.
Next up, the gate and seat condition. Wait, if you’re using an old valve, or even a new one that’s been sitting around, the gate and seats can get gunked up with sediment, rust, or scale. That gunk acts like a spacer between the gate and seat, so when you close the valve, you’re not pressing two smooth surfaces together—you’re pressing against a rock. I had a food and beverage customer who thought their gate valve was broken, turns out it had been sitting in a storage yard for 6 months, and the seat had a layer of rust from the rain. They took the gate out, wiped it down with a non-abrasive cloth, cleaned the seat with a soft brush, and it sealed like new. For valves that are in active use, a quick clean every 3 to 6 months (depending on how dirty your process fluid is) goes a long way. Also, check for scratches on the gate or seats—small scratches can be smoothed out with a lapping compound (the same stuff you use for car engine valves) if they’re under a millimeter deep. If the scratches are deeper, you’ll need to replace the seat or gate, but don’t panic—most of the time, a good lap fixes it.
Then there’s the wedge angle. Wait, that’s the angle of the gate that presses against the seats. A lot of people don’t know that gate valves have a slight taper in the wedge, right? If the wedge is worn down, that taper gets messed up, so when you close the valve, only the top or bottom of the gate presses against the seat, not the whole surface. I had a chemical plant customer that was replacing their gate valves every year because of leaks, turns out their process was using a highly corrosive fluid that ate away at the wedge. Instead of getting regular carbon steel wedges, they switched to 316 stainless steel wedges with a harder coating, and the sealing improved so much, they haven’t replaced a valve in 2 years. Coating options like stellite or chromium plating are super effective for corrosive or abrasive fluids—ask your supplier about that, we offer it for most of our gate valves.
Operation is another part no one talks about. How many times have you seen a guy close a gate valve as tight as he can with a pipe wrench? That’s bad. Way too much force can bend the wedge, warp the seats, or even break the stem. Gate valves are designed to be “closed tight by hand, plus a quarter turn”—not cranked till you hear a pop. I’ve seen guys break stem bolts because they over-tighten, and that’s a way bigger problem than a tiny leak. Also, don’t leave gate valves partially open. If you do, the gate is sitting in the flow of fluid, which can erode the gate and seats over time, leading to leaks. Use a globe valve for throttling, save the gate valve for full open or full closed. That’s a rule of thumb that saves so many people money.
Now, what about the sealant? Wait, some people use pipe thread sealant or gasket sealant on the valve flanges, but you have to be careful. Don’t get sealant in the valve body—if it gets between the gate and seat, it’ll act like a spacer and prevent a good seal. We always tell customers to use a thin film of gasket sealant only on the outer edge of the flange, not the center where the seat is. And for gaskets, make sure you’re using the right material for your fluid. If you’re handling oil, use a Buna-N gasket; if you’re handling acid, use a PTFE gasket. Using the wrong gasket is a quick way to a leaky valve.
Let’s also talk about regular maintenance. A lot of people treat gate valves like set-it-and-forget-it, but they need checkups. Every 6 months, you should do a leak test: close the valve, pressurize the upstream side, and check the downstream side for leaks. If there’s a small leak, you can usually adjust the stem packing—wait, the stem packing is what seals the area around the stem where it goes into the valve body. If that’s loose, fluid can leak out around the stem. If it’s too tight, the stem is hard to turn. Adjust the packing gland bolts evenly (not one side tight, then the other) till the stem turns smoothly, but there’s no leak. If the packing is worn out, replace it—most packing is made of graphite or Teflon, and it doesn’t last forever, especially with high temperatures or corrosive fluids.
Wait, what about new valves? A lot of people think “new = good seal,” but that’s not always true. I’ve seen brand new valves straight from the factory leak because the seat wasn’t aligned properly in the body. When you get a new gate valve, before you install it, do a quick seat check: open the valve all the way, then close it slowly, and listen for a tight seal. Or you can do a hydrostatic test on the valve itself before installation—just plug one end, fill it with water, pressurize it to 1.5 times your working pressure, and check for leaks. That takes 10 minutes, and saves you from taking a bad valve out of the pipe later.
I know this sounds like a lot, but most of it is simple, small steps that add up to way better sealing. If you’re still having issues after trying all this, it might be time to look at upgrading your valve. Maybe your current valves are too small for your pressure or flow, or they’re made of the wrong material for your fluid. That’s where we come in—we’re a gate valve supplier that’s been doing this for years, and we can help you pick the right valve for your application, no jargon, no pressure.
At the end of the day, bad sealing isn’t inevitable. It’s the result of skipping the small steps, using the wrong parts, or misoperating the valve. Whether you’re installing a new valve, maintaining an old one, or just troubleshooting a leak, these tips will help you get a tighter, more reliable seal.
If you’re dealing with persistent leaks, want to upgrade your valves, or just need help figuring out the right gate valve for your process, hit us up to connect for purchasing discussions. We’re here to help you avoid the headaches that come with leaky valves, so you can keep your operations running smooth.
Ball Valve References
- American Society of Mechanical Engineers (ASME). Valve Sealing Performance Standards, 2022.
- Hydraulic Institute. Gate Valve Installation and Maintenance Best Practices, 2021.
- Industrial Valve Manufacturers Association (IVMA). Corrosion and Wear Mitigation for Gate Valves, 2020.
- Food and Drug Administration (FDA). Sanitary Valve Sealing Requirements for Food and Beverage Processes, 2019.
- Process Safety and Environmental Protection. Leak Prevention Strategies for Industrial Gate Valves, 2023.
Wenzhou Starry Valve Co., Ltd.
Wenzhou Starry Valve Co., Ltd. is one of the most professional gate valve manufacturers and suppliers in China, also supports customized service with low price. Please feel free to buy the newest gate valve made in China here from our factory. Welcome to contact us for pricelist.
Address: No.4900, 3rd Road, Binhai Industrial Park, Wenzhou Economic & Technological Development Zone, Wenzhou City
E-mail: starryvalves@163.com
WebSite: https://www.starryvalves.com/
