If you’ve ever stood in front of a heavy-duty band saw machine, the kind that’s seen 10,000 cuts through steel, wood, or even composite materials, you know it’s equal parts workhorse and potential hazard. Over the past 12 years as a band saw machine supplier, I’ve watched hundreds of new operators (and even some seasoned ones) make small, avoidable mistakes that turn a smooth cut into a ruined piece of stock, a damaged blade, or worse—a trip to the shop clinic. I’ve seen a guy ruin a $2,000 titanium block because he skipped a blade tension check, and another bend a machine table so bad it took two weeks to repair just because he rushed a thick aluminum cut. These mistakes aren’t random; most are rooted in assumption, rushing, or assuming “that’s how we’ve always done it” instead of stopping to check the basics. Today, let’s talk about the common errors I see again and again, so you can keep your cuts clean, your blades sharp, and yourself safe. Band Saw Machine
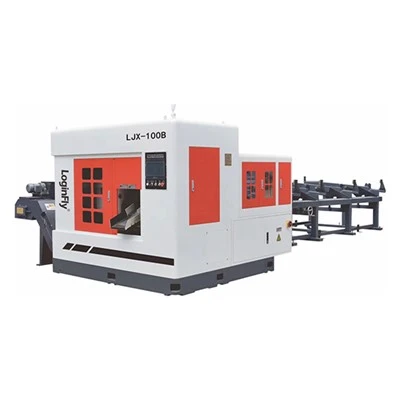
The first mistake, and the most frequent I encounter, is ignoring proper blade tension. I can’t tell you how many times a new customer will call me upset because their blade snapped mid-cut, only to pull up their maintenance log and see they last checked tension three months prior. Band saw blades aren’t one-size-fits-all when it comes to tension: a 14 TPI (teeth per inch) blade for cutting hardwood needs 15,000 PSI of tension, while a 24 TPI blade for thin sheet metal needs 18,000 PSI—too little tension makes the blade wander or twist, too much makes it stretch and snap prematurely. I once had a regular customer who swore by “eyeballing” tension for years, until a blade shattered and chipped the machine’s upper guide, costing him $800 in parts and downtime. The fix is simple: use the built-in tension gauge on your machine, or a portable tension meter, every time you install a new blade. Don’t rely on how tight the lever feels—that’s a personal guess, not a scientific measurement.
Next, skipping blade guide alignment. This is a tiny adjustment that makes a world of difference, but almost every new operator I train bypasses it. Blade guides are the small, adjustable blocks on either side of the blade that keep it from swaying as it cuts. If they’re misaligned—even by a millimeter—you’ll get crooked cuts, and the blade will rub against the guide instead of cutting through material, causing excessive heat and premature dulling. I watched a shop last year that cut 50 pieces of 2-inch steel incorrectly, all because the night shift operator forgot to reset the guides after changing a blade. They wasted two full days re-cutting stock, which meant missing a delivery deadline and losing a client. The rule here is straightforward: after every blade change, and before any cut thicker than half an inch, stop and adjust the guides so they’re just brushing the back of the blade, not pinching it. Pinching creates friction that wears the blade down fast, and too much space lets it sway.
Third, using the wrong blade for the job. This is such a simple mistake, but it’s shocking how often it happens. Last quarter, a carpenter came to my shop furious because he’d ruined a $500 band saw blade trying to cut a 6-inch steel I-beam with a 10 TPI blade meant for soft pine. Blades are designed for specific material types and thicknesses: TPI is the biggest factor here. For wood or soft metal, low TPI (6–10) is best because fewer teeth mean bigger gullets to clear wood chips or metal shavings, preventing clogs. For thin sheet metal, plastic, or small metal parts, high TPI (18–32) works better because more teeth create smoother cuts without bending. If you use a low TPI blade on thin metal, the teeth will catch and break. If you use a high TPI blade on thick steel, the teeth will drag and overheat, dulling in minutes. I always tell customers to remember the general rule: thicker material = lower TPI, thinner material = higher TPI. And if you’re cutting a mix of materials (like a steel frame with aluminum brackets), pick a variable TPI blade—it’s designed to handle both without switching blades constantly.
Fourth, not securing your work piece properly. I’ve seen this mistake lead to everything from ruined cuts to broken machines. A few months ago, a hobbyist tried to cut a 4-foot pine plank freehand, no vise or hold-down, and the plank slipped mid-cut, slamming into the blade guard and bending the blade at a 45-degree angle. The repair cost him $1,200, plus he missed his weekend project deadline. Even if you’re using a small band saw for hobby work, never hold material by hand when cutting thicker than 1 inch. Vises, clamps, or hold-downs aren’t just suggestions—they’re safety tools. For large pieces, use the machine’s built-in fence to keep the material aligned, and make sure it’s tightened down so it can’t shift. Another common mistake here: cutting a piece that’s too long and hanging off the back of the table without support. That overhang puts stress on the blade and table, leading to crooked cuts or even the table tilting over time. If you’re cutting a long piece, use a roller stand or another worker to support the end as it comes off the saw.
Fifth, rushing the feed rate. Feed rate is how fast you push the material into the blade, and it’s tempting to go fast to get the job done—but that’s a recipe for disaster. I once had a production shop push so fast cutting ½-inch aluminum that the blade overheated so much it discolored, and the cut surface was so rough they had to sand each piece individually, adding 30 minutes per part to their workflow. Too slow, and you’ll get the opposite problem: the teeth will rub instead of cut, generating heat and dulling the blade. The right feed rate depends on the material: for wood, a moderate push (about the speed you’d draw a line with a pencil) works. For steel, a slower, steady feed, just enough to hear a consistent hum from the blade, is best. For thin metal, you need an even slower feed, because high pressure will bend the material or snap the blade. If your blade starts to smoke or make a high-pitched whine, you’re feeding too fast—stop, back off, and adjust.
Sixth, ignoring regular maintenance of the saw itself, not just the blade. A band saw is like a car: you can’t go 10,000 miles without an oil change, and the same goes for your saw. I see shops that run their machines 12 hours a day, 6 days a week, without cleaning the chip pan, lubricating the blade guides, or checking the blade tracking. Blades that aren’t tracked properly (meaning they’re aligned straight on the upper and lower wheels) will run off-center, causing excessive wear on the side of the blade and leading to breaks. Chip pans full of shavings can get sucked up into the motor, causing overheating and motor failure—one shop I work with had to replace a motor because they never emptied the chip pan, costing them $2,500 in downtime and parts. Every two weeks, wipe down the saw table, empty the chip pan, and check the wheel bearings for any looseness. Every six months, have a technician check the blade tracking and adjust it if needed—most of our regular customers get this as part of our maintenance support when they buy a machine from us, because we know how much it matters.
Another mistake that’s easy to miss: not wearing the right personal protective equipment (PPE), or wearing the wrong kind. I’m a firm believer in safety, but I’ve seen new operators come to our shop wearing baggy flannel shirts, necklaces, or even gloves while running a band saw. Those loose items can get caught in the blade in a split second, leading to serious injury. Gloves are especially a no-no for band saw use—they can snag on the blade and pull your hand in. Instead, wear tight-fitting clothes, safety glasses (chips fly even with a guard in place), and closed-toe shoes. If you have long hair, tie it back in a ponytail or under a hard hat so it can’t catch on the upper wheel. This isn’t just a “rule”—it’s a small step that can prevent a life-altering accident.

I know a lot of these mistakes sound basic, but in my 12 years selling band saw machines, I’ve seen every single one play out in real, expensive ways. The good news is that almost all of them are avoidable with a little attention to detail, a quick pre-cut check, and not cutting corners on maintenance or safety. If you’re in the market for a new band saw, or looking to upgrade your current setup to reduce blade breakage and downtime, our team can help you pick the right machine and blades for your specific needs, plus walk you through a simple maintenance routine tailored to your workflow. We also offer on-site training for teams that want to reduce these common mistakes and get the most out of their band saw investment. Don’t let small errors turn into big headaches—reach out to our team to chat about your band saw needs, and let’s make your cutting process smoother, safer, and more efficient.
High Speed Circular Saw Machine References:
- Occupational Safety and Health Administration (OSHA). "Power Tool Safety: Band Saws." U.S. Department of Labor, 2022.
- American National Standards Institute (ANSI). "Safety Requirements for Metal-Cutting Band Saw Machines." ANSI B10.15-2020, 2020.
- Groover, M.P. Fundamentals of Modern Manufacturing: Materials, Processes, and Systems. 7th ed., John Wiley & Sons, 2020.
- Carpenter Technology Corporation. "Guidelines for Band Saw Blade Selection and Maintenance." 2021.
- Machinery Lubrication Magazine. "Band Saw Maintenance Best Practices for High-Volume Operations." No. 18, 2022.
Shanghai Loginfly Sawing Technology Co., Ltd.
As one of the most professional band saw machine manufacturers and suppliers in China, our products have good reputation in the market. We warmly welcome you to wholesale premium band saw machine from our factory. If you have any enquiry about cooperation, please feel free to email us.
Address: Room 506 NO.655 Yinxiang Road,Nanxiangtown,Jiading District, Shanghai.China
E-mail: sales01@loginfly.com
WebSite: https://www.loginflysaws.com/
